
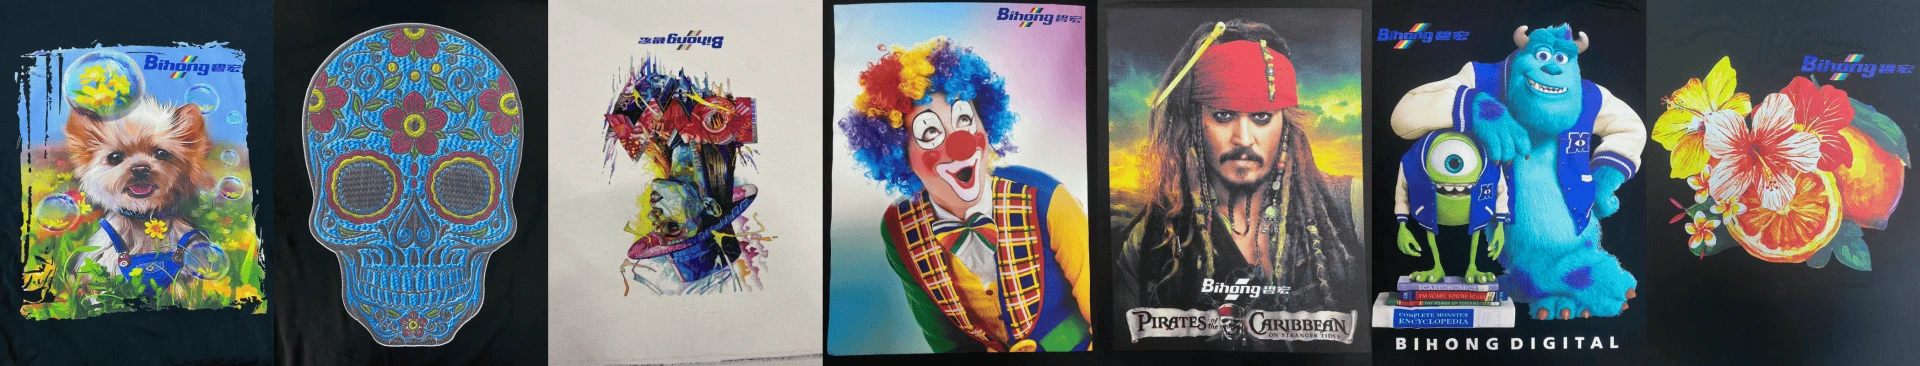
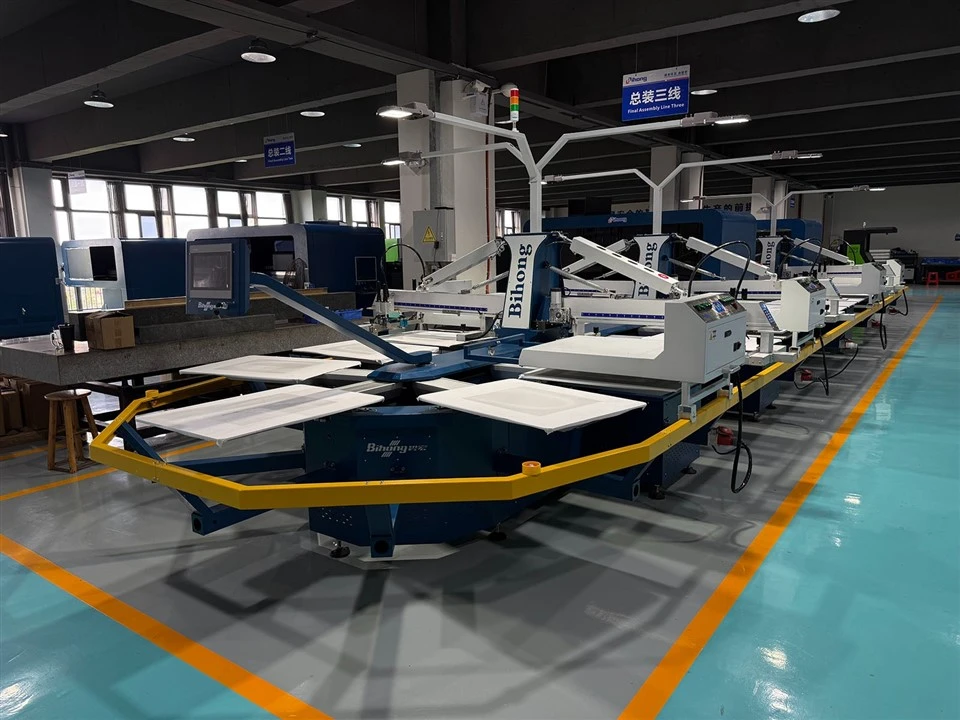
Guangdong Aces Machinery Co., Ltd. is one of the leading manufacturers and suppliers of 6 colors automatic oval screen printing press in China. With abundant experience, we warmly welcome you to wholesale the newest 6 colors automatic oval screen printing press from our factory. All customized machines are with high quality and low price. Welcome to contact us for quotation.
6 Colors Automatic Oval Screen Printing Press Key Features
1. High positioning Automatic t shirt printing press accuracy: self-created triangular positioning system, advanced technology, mature and stable, the positioning accuracy error is within ±0.01 mm, ensuring the positioning accuracy of the pallets and improving the printing quality.
2. Flexible and changeable flash cure: ①Fixed hanging version ②Movable version.
3. Customized models: special models can be provided according to the printing process requirements of different materials for customers. Columns can also be designed to wrap in the machine to make reasonable use of space.
4. Ensure the stable operation of the large version: Dual rails support big pallets.
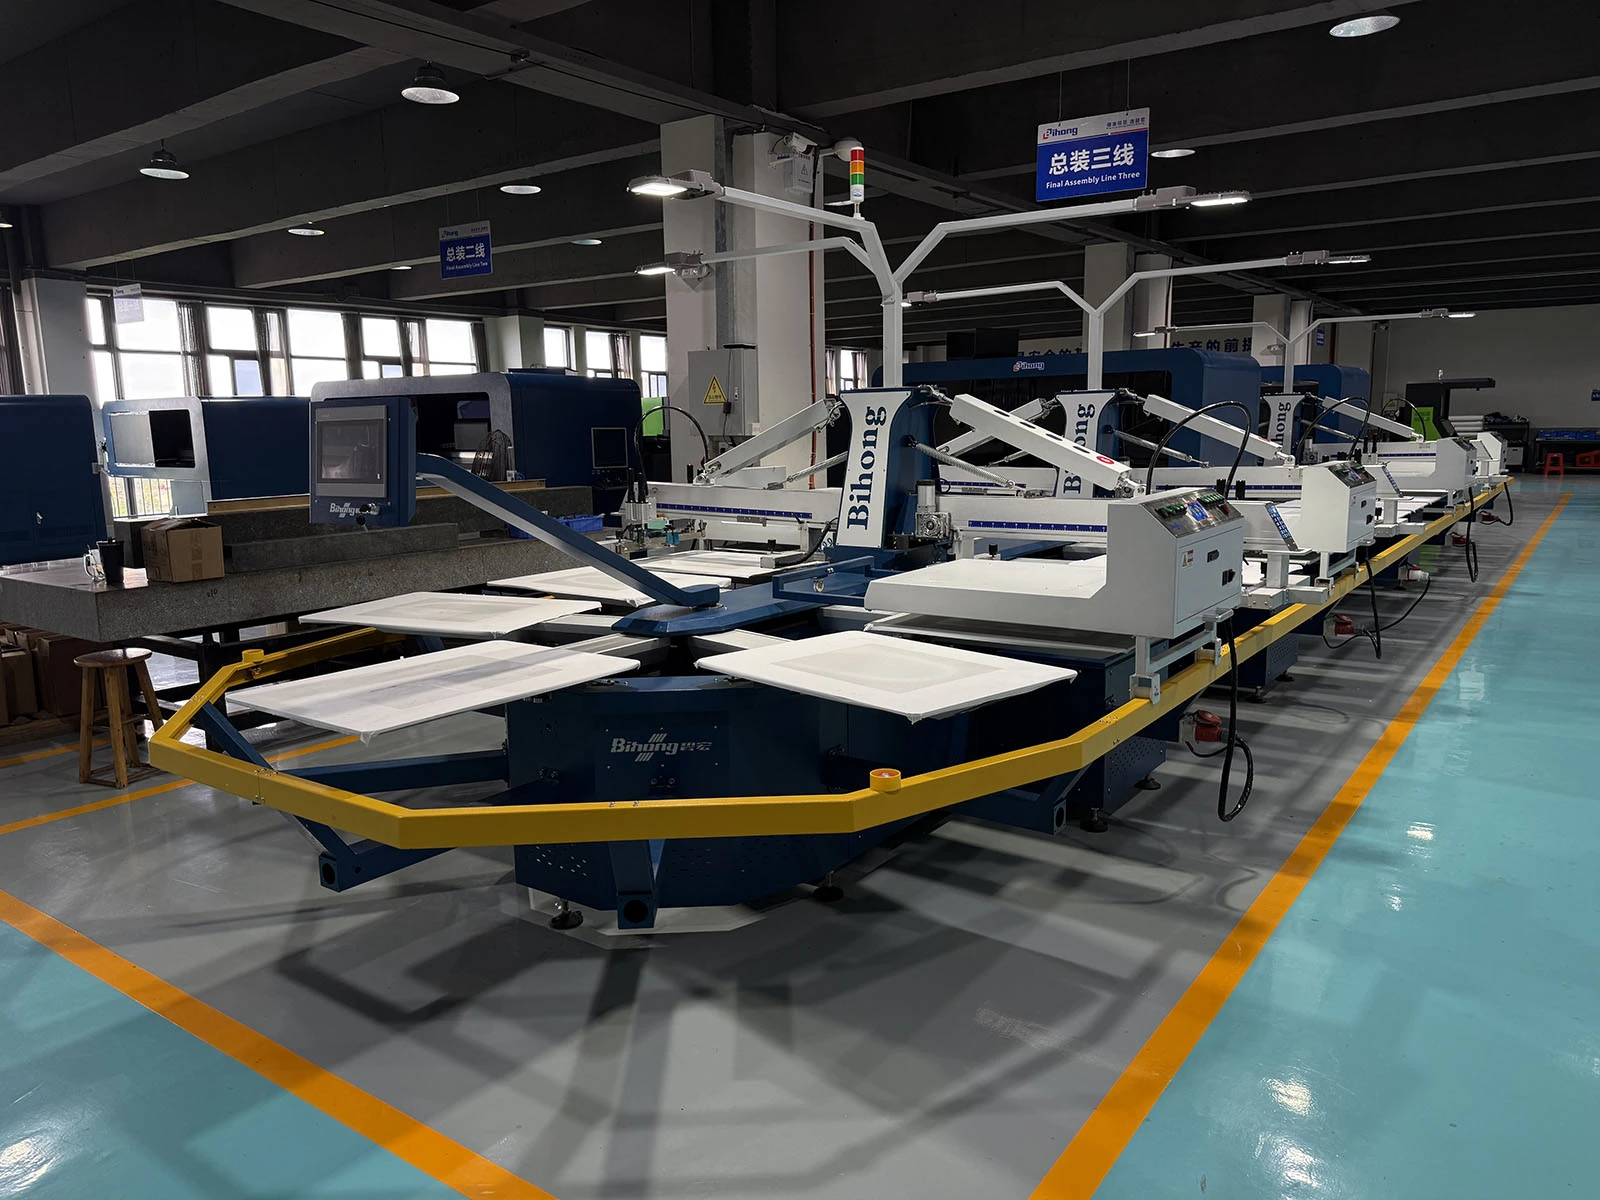
5. Flexibility of screen frame to move: Air-assisted rear frame support facilitates quick screen loading and unloading ;Digital control screen printer Different screen sizes can be used.
6. The operation is more convenient: the screen frame is fixed in a unique way; adopting pneumatic way to lift screen, which saves time Screen Printing Press and labor. Cleaning the screen without picking up the screen.
7. The machine supports various screen frames with no restriction on screen frame dimensions. Customers existing screen frames, whether originally used for automatic machine printing or manual screen printing, are compatible with this equipment. It enables printing on large substrates and garments without size limitations.
8. 6 colors Automatic Oval Screen Printing Press have 24 plates , normally for the regular style printing , it's product volume is about 550-700pcs per hour, basically need 4 workers to manipulate, 1 feeding the fabric cutting , 1 collecting the fabric cutting, 1 machine driving , 1 do cleaning and screen making and odd jobs.
Detailed Standard Operating Procedures
1. Fabric Pre-treatment
1. All sweatshirt and sportswear fabrics must be fully pre-shrunk to eliminate fabric shrinkage tension and prevent 3D pattern deformation and registration deviation after multi-layer printing.
2. Strictly inspect fabric surface: no oil stain, no floating hair, no yarn knots, no uneven cloth surface. Floating hair must be removed by air blowing or brushing to avoid surface pits and bubble points on stereo patterns.
3. Keep fabric flat and stable; avoid elastic fabric stretching during loading, which will cause uneven paste thickness and inconsistent stereo height.
2. Screen Preparation (Key for 3D Effect)
1. Mesh selection: Adopt 60T–80T thick high-tension mesh. Low mesh count ensures large paste carrying capacity, which is the basic condition for thick-layer stereo forming.
2. Emulsion coating: Apply thick emulsion coating 2–3 times to form thick stencil film, increase paste storage capacity, and support multi-layer thick stacking.
3. Screen inspection: Ensure the pattern area is smooth and flat, no pinholes, no residual glue, no mesh blockage. The edge of the pattern must be neat and straight to ensure 3D pattern contour sharpness.
4. Install screen frame stably, adjust horizontal level and off-contact gap to 2.5–4mm, adapt to thick paste printing, prevent paste overflow and edge burrs.
- High-Density Thick Paste Mixing (Core Process)
1. Use special high-density stereo thick base paste as the main material, add color thick paste according to color standard, and stir at low speed evenly.
2. Add a small amount of anti-bubble agent and thickener appropriately to improve paste leveling and stacking performance, prohibit excessive water addition to avoid paste dilution and collapse after printing.
3. Stirring time: 10–15 minutes, until no color particles, no paste delamination, uniform consistency.
4. Viscosity standard: 8000–12000 cps (high viscosity state), ensure the paste has strong support force and will not collapse after thick-layer printing.
5. Filter the mixed paste with 80-mesh filter screen to remove particle impurities and avoid surface protrusion defects of stereo patterns.
6. Paste should be used within 8 working hours; avoid long-term placement leading to viscosity change and affecting stereo forming effect.
- Oval Machine Multi-Layer Printing Parameter Standard
Unified Parameter Standard for Thick 3D Printing
1. Squeegee hardness: 70–75° high-hardness blade
2. Squeegee pressure: Medium-high pressure, uniform force, ensure full paste filling of mesh holes
3. Squeegee speed: 200–300mm/s (slow speed for full paste discharging)
4. Squeegee times per layer: 2 strokes (one forward, one backward) to ensure full and uniform paste stacking
5. Printing layers: Conventional 3–4 layers stacking (adjust according to customer required stereo height)
6. Inter-layer drying temperature: 90–110℃, single-layer drying time 60–90s
7. Final curing temperature: 120–130℃, curing time 3–5min (ensure layer adhesion and stereo shaping firmness)
3. Layered Printing & Inter-Layer Drying Standard (Most Critical Step)
1. First layer printing: Print the base layer evenly, dry thoroughly at 90–110℃, ensure the base layer is fixed without sticking, lay a flat foundation for subsequent stacking.
2. Second & third layer over-printing: Strictly align registration, repeat printing according to standard squeegee parameters, and perform full drying after each layer. It is forbidden to stack multiple layers without drying, which will cause internal bubbles, layer delamination and final collapse.
3. According to the required 3D stereo height, complete 3–4 layers of cyclic printing and drying to form uniform raised thickness.
4. After the last layer of printing is completed, perform high-temperature integrated curing to stabilize the stereo shape, enhance paste elasticity and fabric adhesion.
- First Article Confirmation (Mandatory)
1. After parameter debugging and layered printing, produce the first finished sample.
2. QC inspection items: pattern registration accuracy, 3D stereo height uniformity, surface smoothness, no bubble, no crack, no edge collapse, neat pattern contour.
3. Hand feel test: obvious raised stereo embossed feeling, solid texture, elastic and non-brittle.
4. Adhesion test: Use 3M tape to stick and tear repeatedly, no layer peeling, no falling off.
5. After the first article is signed and confirmed by QC and production supervisor, mass production can be started.
- Mass Production Operation Standard
1. The fabric is laid flat and positioned accurately to ensure consistent printing position of each piece and no offset.
2. The operator strictly follows the fixed number of printing layers, drying temperature and drying time, and does not arbitrarily speed up the production rhythm to avoid incomplete drying.
3. Check the screen mesh condition every 30 minutes to prevent mesh blockage and insufficient paste output leading to uneven stereo height.
4. Keep the paste slightly stirred during production to prevent precipitation and ensure consistent color and thickness of each batch of patterns.
5. Patrol inspection focuses on: stereo height consistency, surface bubble defect, edge flatness and layer firmness.
4. Finished Product Inspection Standard
1. 3D Stereo Effect: Uniform raised height, full embossed texture, three-dimensional and fashionable, no local collapse or depression.
2. Surface Quality: Smooth and flat pattern surface, no bubbles, no cracks, no particle pits, neat and clear edge contour.
3. Adhesion Performance: No delamination, no peeling after tape adhesion test.
4. Washing Fastness: No falling off, no cracking after conventional water washing test.
5. Overall Appearance: Uniform color, no color difference, consistent stereo effect in batch.
- Quality Acceptance Standard
1. Stereo height meets customer sample standard, uniform thickness in the whole batch.
2. The printed pattern has strong 3D embossed sense, solid texture and good elasticity.
3. Zero bubble, zero crack, zero collapse on the pattern surface.
4. Firm adhesion, no delamination between layers, excellent washing and rubbing fastness.
5. Batch defect rate is controlled within factory standard range.
Common Defects, Causes & Corrective Actions
|
Defect Phenomenon |
Root Cause |
Corrective Action |
|
3D pattern collapse & flatness |
Paste viscosity too low, inter-layer drying insufficient, too fast stacking speed |
Increase paste viscosity, extend inter-layer drying time, strictly implement layer-by-layer drying |
|
Pattern surface bubbles |
Paste stirring with air, no defoaming, insufficient drying |
Add anti-bubble agent, stir slowly, stand for defoaming before use |
|
Layer delamination & peeling |
Incomplete curing, uneven paste adhesion |
Improve final curing temperature and time, stabilize paste formula |
|
Uneven stereo height |
Unstable squeegee pressure, inconsistent paste output |
Calibrate machine parameters regularly, keep paste uniform |
|
Pattern edge burrs |
Screen gap too large, paste too thin |
Adjust screen off-contact gap, increase paste viscosity |
|
Post-washing crack |
Excessively thick single layer, insufficient elasticity |
Increase printing layers appropriately, reduce single-layer paste volume, improve paste elasticity |
Safety & On-Site Management Specifications
1. High-density thick paste contains high-viscosity chemical components; the workshop must maintain good ventilation.
2. Strictly control the temperature of the drying tunnel to prevent high-temperature baking and scorching of fabrics and printed layers.
3. Clean the screen and squeegee with water in time after shutdown to prevent thick paste from drying and blocking the mesh.
4. Operators must wear protective gloves to avoid long-term direct contact with printing paste.
5. Waste paste and wastewater shall be disposed in accordance with environmental protection standards, and random dumping is prohibited.
Production Record Documents
High-Density Paste Mixing Record
First Article Inspection Report
Machine Parameter Setting Record
Production Process Patrol Log
Finished Product Quality Inspection Record
Hot Tags: 6 colors automatic oval screen printing press, China 6 colors automatic oval screen printing press manufacturers, suppliers, factory


